
Advantages of laser welding
The advantage of laser welding
is in your hands
With laser welding, you can achieve up to 10× faster welding speeds, significantly boosting productivity and profitability.
Laser or traditional welding?
This shouldn’t be a question
Traditional welding asks a lot of the welder: several passes, a lot of heat in the part, and rework once the seam is done. Laser welding takes most of that away.
A THEO laser welder is up to 10× faster than TIG. The heat input is low, so parts distort less and keep their strength. The melt pool is uniform, so seams come out consistent from one part to the next.
You also use less: less filler, fewer consumables, less electricity. The table below shows the differences row by row.
Traditional and THEO laser welding compared
No comparison, really.
| Traditional welding | THEO laser welding | |
|---|---|---|
| Speed | Slower processing times, often requiring multiple passes. | Up to 10× faster than TIG. |
| Precision | Moderate precision, with higher reliance on operator skill. | Superb accuracy, ideal for small parts and thin gauge applications. |
| Waste reduction | High material waste due to excess filler and slag. | Minimal waste, fewer consumables, and environmentally responsible. |
| Heat impact | Higher heat input, increasing the risk of warping or fatigue. | Low heat input: minimal distortion and preserved material strength. |
| Cost efficiency | Consumables and labor hours increase operating costs. | Significant long-term savings and reduced operating costs. |
| Welding seam damage | Potential for porosity, lack of consistency. | Uniform melt pool and great consistency. |
| Environmental impact | High emissions, energy-intensive, and more consumable waste. | Lower electricity consumption, lower overall costs. |
| THEO laser welding | Traditional welding | |
|---|---|---|
| Speed | Up to 10× faster than TIG. | Slower processing times, often requiring multiple passes. |
| Precision | Superb accuracy, ideal for small parts and thin gauge applications. | Moderate precision, with higher reliance on operator skill. |
| Waste reduction | Minimal waste, fewer consumables, and environmentally responsible. | High material waste due to excess filler and slag. |
| Heat impact | Low heat input: minimal distortion and preserved material strength. | Higher heat input, increasing the risk of warping or fatigue. |
| Cost efficiency | Significant long-term savings and reduced operating costs. | Consumables and labor hours increase operating costs. |
| Welding seam damage | Uniform melt pool and great consistency. | Potential for porosity, lack of consistency. |
| Environmental impact | Lower electricity consumption, lower overall costs. | High emissions, energy-intensive, and more consumable waste. |
Swipe sideways to compare →
Why it works
Why the heat stays where you want it
A laser puts a lot of energy into a very small spot. The metal at that spot melts quickly and the weld is narrow, so only a small volume of metal is heated. Much less heat spreads into the part around the seam.
Less heat in the surrounding metal means a narrower heat-affected zone, the strip next to the weld where the metal’s structure changes. That is why the part is less likely to warp.
This is a property of the process, not of one machine. Your result still depends on settings and technique.
Distortion
Less distortion means less rework
When a part moves during welding, you spend time afterwards on straightening, fitting and finishing. A process that puts less heat into the part gives you less of that to do. You see it most on thin sheet.
The same goes for the seam. A weld made with the MA1 needs almost no grinding or polishing.
What is left depends on the job: seam appearance, oxide color and what your customer accepts.
Materials and thickness
Know the penetration of your machine
Laser welding is known for thin sheet, where low heat input keeps the metal flat. How deep you can weld depends on laser power.
With the MA1 Series, weld penetration in stainless steel runs from 3.5 mm on the MA1-35 to 8.5 mm on the MA1 ULTRA. Those figures are weld penetration, not the thickness of the sheet you can join.
Training
Skill still matters, in a different way
A laser does not remove the need to learn the process. TWI, the UK welding research institute, notes that the welder’s skill and the laser’s characteristics together shape the weld profile and the defects you get.
What changes is how long it takes. Operators train on the MA1 in hours and reach proficiency in 1 to 2 weeks.
Plan for training anyway. A short learning curve is a benefit, not a reason to skip it, and some countries, Germany among them, require a designated laser safety officer.
Fit-up
Fit-up decides how good the weld is
A laser beam is small, so it is less forgiving of gaps between parts than an arc. If the edges are cut and held well, you get the benefits above. If the gap varies along the seam, quality drops.
There are ways to widen the margin. The MA1 torch has a wobble function that moves the beam for a wider weld: up to 4 mm (0.16 in), and 6 mm with the Dual Wire Feeder. A wire feeder adds filler to bridge gaps.
As a rule of thumb, with filler wire you can bridge a gap of up to about 80% of the wobble width. That is roughly 3 mm with the T1 Wire Feeder. For the Dual Wire Feeder we state 4 mm, on the safe side of the rule. It is a rule of thumb, not a tested limit, so try it on your own joint first.
So the saving starts before welding: consistent cutting, bending and clamping. Shops that already hold tight fit-up get the most from laser welding.
The honest part
Where laser welding is not the best choice
Laser welding is not the answer to every job. Consider another process when:
- The joint has poor fit-up. Large or uneven gaps and parts that move during welding favor an arc process.
- The metal is thicker than your machine welds. Each MA1 model has a weld penetration limit, up to 8.5 mm in stainless steel on the MA1 ULTRA.
- The metal is highly reflective. Aluminum reflects much of the beam and conducts heat away fast. The MA1 Series welds it, but expect more testing and settings work than with stainless steel.
- You cannot give it the safety setup. The MA1 is a Class 4 laser product. It needs laser eye protection for everyone in the area and a controlled room or laser curtains.

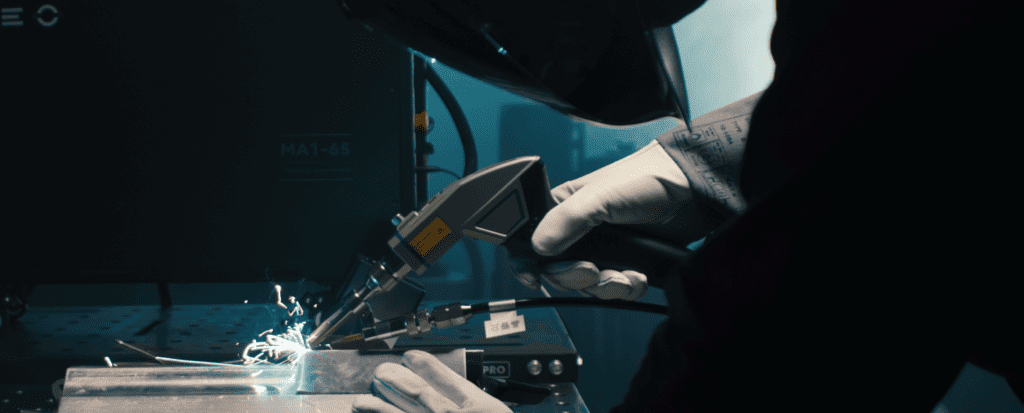
THEO MA1
The Time Saver
From the blog
Read more on our blog

Laser Welding Unit Converter: Gauge, Speed, Gas and Power (+ FREE THEO Shop Math)
Your print says 16 gauge. Your wire box says .035. Your flowmeter reads CFH. Your laser welder wants millimeters, millimeters per second,…
November 12, 2026

What is Nominal Ocular Hazard Distance? A Guide (+ FREE THEO NOHD Calculator)
A laser welding beam stays dangerous to your eyes over a surprisingly long range, and the figure that defines said range is the Nominal Ocular Hazard…
September 4, 2026

The Skeptic’s Guide to Buying a Laser Welding Machine [2026]
If you weld for a living, a healthy dose of doubt is an asset, not a flaw. So, when a handheld laser welding machine…
July 27, 2026
Laser welding
Keep reading
Talk to THEO
Select the perfect handheld laser welding machine for your needs.
